
ECK6120A/B Oval Turning Machine
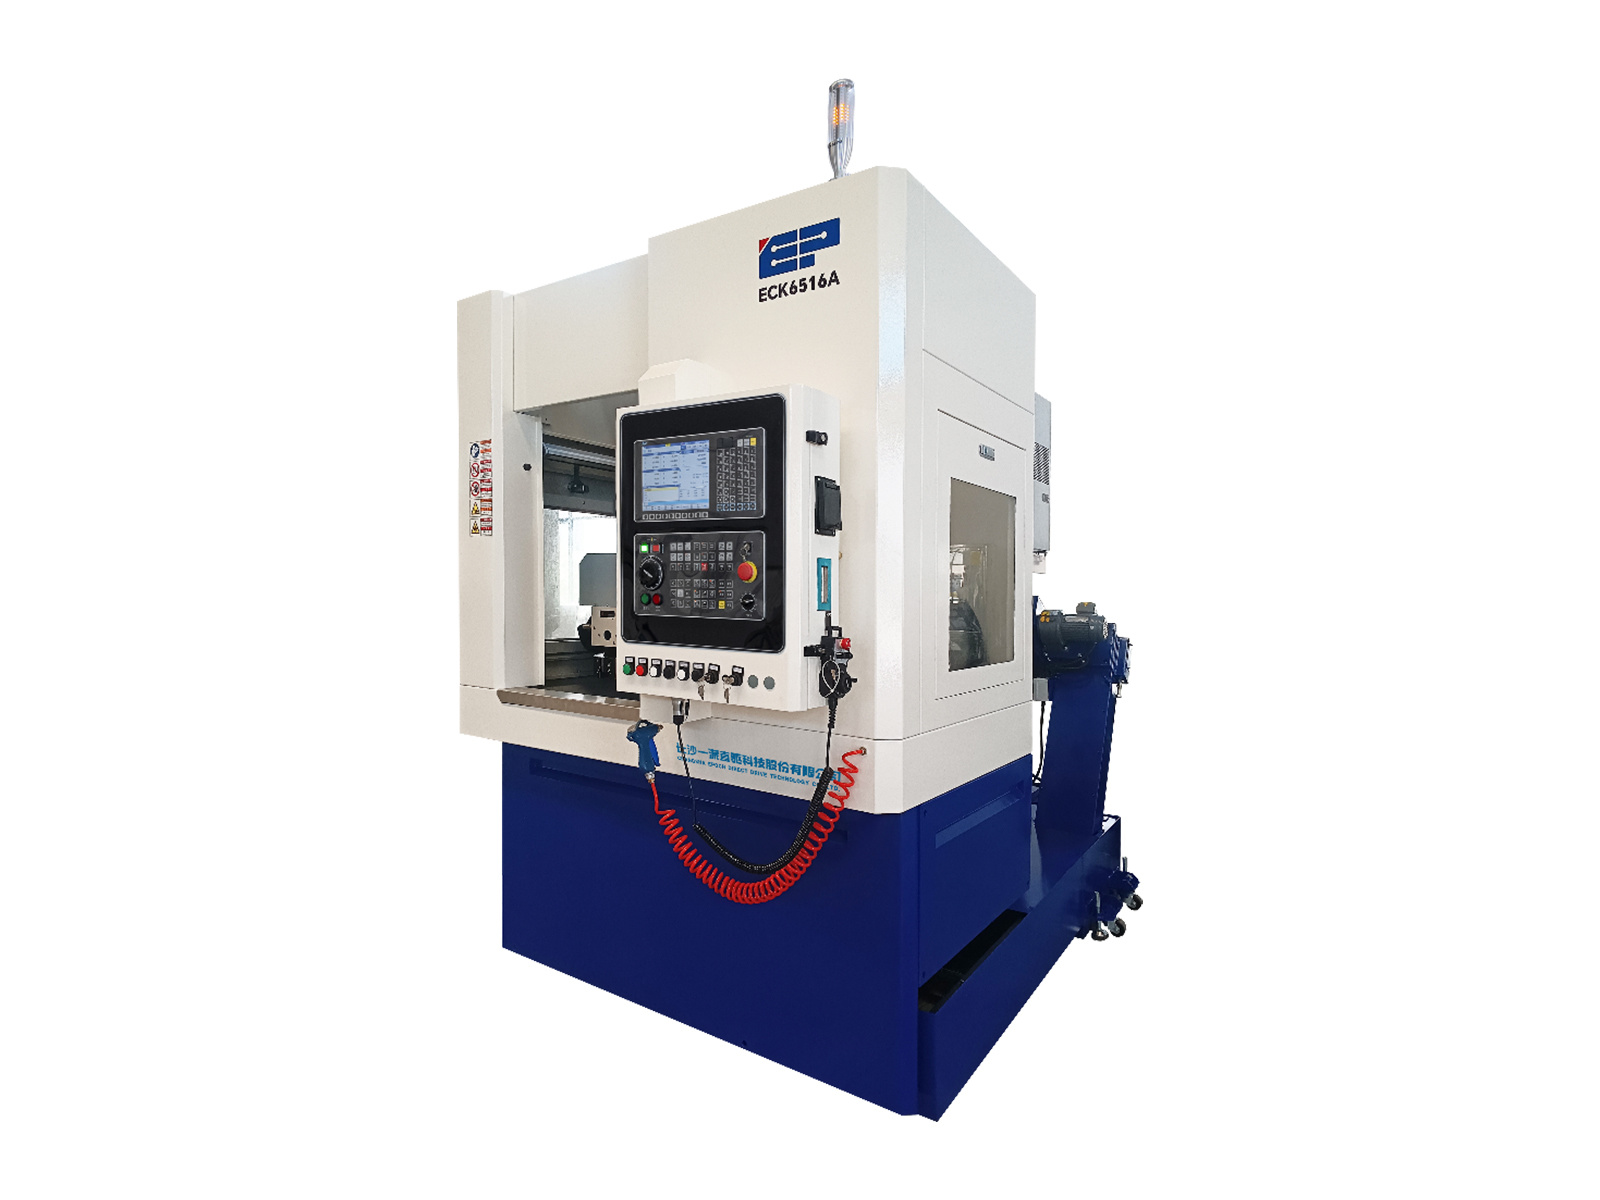
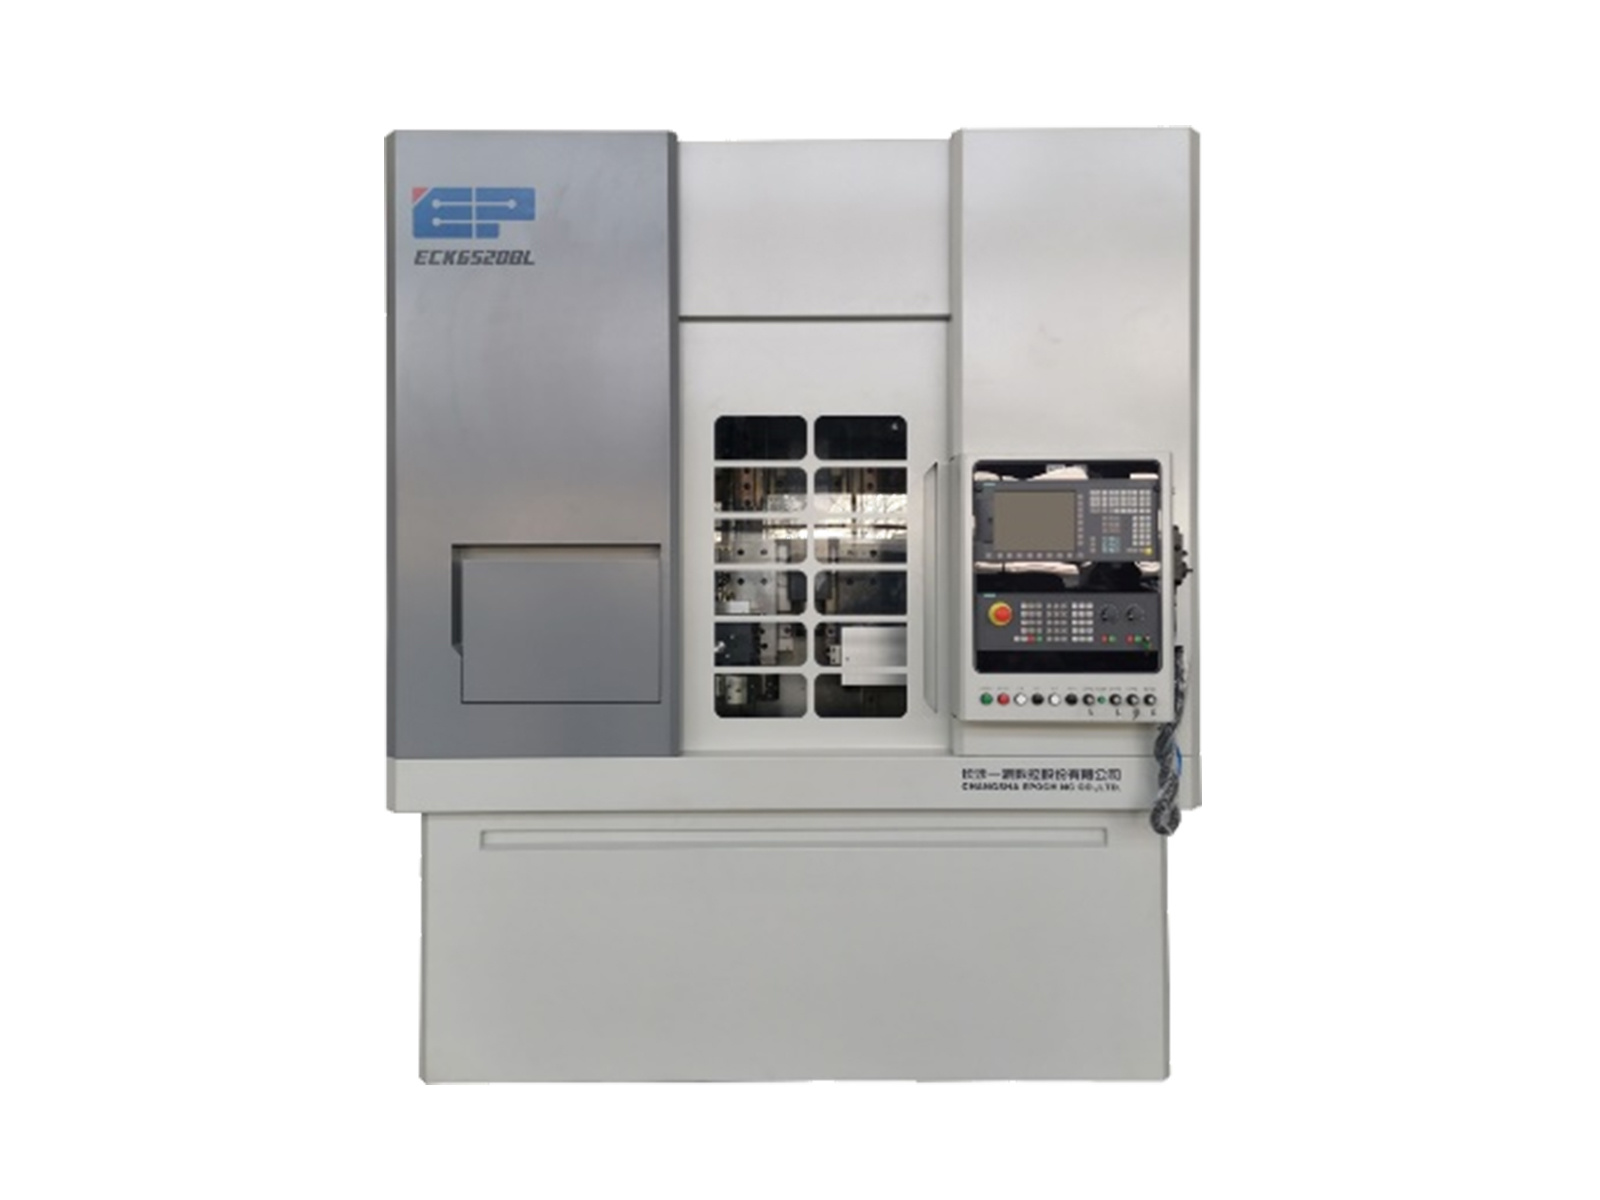
The machine tool adopts a horizontal integral flat bed structure, mainly used for machining steel piston irregular outer circles;
The software is powerful and can edit various irregular outer circles required by the piston, including standard ellipses, ellipse superimposed eccentric circles, eccentric ellipses, rotating ellipses or discrete data fitting, etc.;
Tightening or clamping devices can be selected according to customer requirements.
- Technical Parameter
- Describe
-
- Commodity name: ECK6120A/B Oval Turning Machine
Serial Number Item Unit ECK 6120A ECK 6120B 1 Piston Diameter mm Φ80~Φ200 2 Piston Length mm 80~200 3 Spindle Type A2-8 bearing spindle 4 Spindle Accuracy mm 0.003 5 Spindle Speed rpm 50~2000 6 Linear Servo Tool Post Flat linear servo tool post system EJX1260A 7 Numerical Control System SIIMENS 828D 8 Linear Motor Stroke mm 6 9 Linear Motor Repeat Positioning Accuracy mm 0.0003 10 Maximum Workpiece Ovality (Diameter) mm 4.0 11 Maximum Workpiece Profile (Diameter) mm 4.0 12 Machining Roughness μm Ra0.8 13 X-axis Drive Mode Manual Servo drive closed-loop control 14 Process Capability Index ΦD±0.015mm CmK≥1.33 15 Main unit (length × width × height) mm 2355×1938×2043 16 Net weight of main unit kg 5500 17 Total power Kw 30 -
Main Machine Configuration:
1. Basic ComponentsThe machine's base, slide, spindle housing, and other basic components are made using high-strength casting technology, resulting in a stable internal microstructure. The casting structure has undergone machine dynamics analysis and finite element analysis to optimize its geometry and ensure high rigidity. The wide and sturdy machine base, with its full-support load design, adheres to advanced material mechanics design principles, ensuring load capacity during machining.
2. High-Precision Spindle UnitUtilizes a high-precision bearing spindle with stepless frequency conversion speed control, offering high accuracy, long lifespan, and easy maintenance.
3. Spindle Circular GratingSpindle positioning uses a Heidenhain ERM2400 circular grating instead of the original encoder and synchronous belt structure, achieving a positioning accuracy of ±7.5″, effectively improving the piston outer circle knurling condition.
4. Linear AxisThe X/Z axes use high-precision ball screw pairs and imported high-precision linear rolling guides. The ball screw employs a pre-tensioned assembly process, significantly increasing transmission rigidity and eliminating thermal deformation during high-speed movement, thus ensuring the machine's positioning accuracy, repeatability, and stable machining accuracy. The imported high-precision linear grating scale installed on the Z-axis provides the Z-axis position signal for the dedicated linear servo tool post driver. The X-axis uses closed-loop control, achieving high positioning accuracy and allowing adjustment of the linear servo tool post position via the control system.
5. Linear Servo Tool Post(1) The self-developed new generation flat linear servo tool post EJX1260A has reached internationally advanced levels. This tool post boasts extremely high dynamic accuracy, dynamic stiffness, and frequency response. Its output force reaches 1500N, stroke ±3mm, frequency response exceeds 450Hz/-3dB, and repeat positioning accuracy is as high as 0.0003mm;
(2) Uses a self-developed high-precision servo driver EHA3020T0S with dual CPU control, achieving a servo frequency of up to 16K. Data processed by dedicated software can be downloaded to the dedicated driver to control the machining of the piston's irregularly shaped outer circle.

6. Numerical Control (NC) and Electrical Control Systems
(1) Employs the internationally standardized Siemens 828D numerical control system, which is simple to operate and highly reliable;
(2) Wiring within the electrical cabinet complies with national electrical safety standards, ensuring the control system is not affected by external interference during operation. An air conditioner is used to quickly exhaust hot air from the electrical cabinet, maintaining a constant temperature and ensuring long-term stable operation of the control system.
7. Machine Software(1) The "Epoch Piston Surface Data Processing Software" can edit and control various irregular circumferences required for piston machining, including standard ellipses, ellipse-superimposed eccentric circles, eccentric ellipses, rotated ellipses, or discrete data fitting. Its interface is clear, intuitive, user-friendly, and easy to operate.
(2) Piston surface data input adopts a chart-based interface, making data entry visually straightforward. Cross-sectional shape data is displayed using polar coordinate graphics, providing an at-a-glance overview.
(3) Upon completing data input, the software automatically calculates and displays the contour diagram, facilitating verification.
(4) The machining software features simplified parameter input and a user-friendly man-machine interface. It monitors and displays the entire machining process status in real time.
8. Lubrication System
An automated timed and metered lubrication system (with adjustable flow) delivers oil to moving components including guideways and ball screws. This minimizes oil waste while providing an environmentally friendly solution.
9. TailstockA pneumatic cylinder drives the tailstock sleeve movement to extend or retract the center point, with speed regulated by two cylinder flow control valves. To accommodate various piston types, the tailstock body features adjustable positioning, ensuring machining accuracy with user-friendly and reliable operation.
10. ToolingUses the piston mouth as the positioning datum. The machine provides two methods for clamping the piston: one is pneumatic clamping by the tailstock; the other is spring clamping with pneumatic release. Users can choose according to their process requirements.
11. OthersThe machine is equipped with a fully enclosed protective cover, a high-flow cooling system, and is aesthetically pleasing, safe, and leak-proof. The chip removal device is simple, environmentally friendly, practical, and reliable.
Direct Drive Business:86 181-6366-2916 (Manager Jiang)
Machine Tool Business:86 150-7465-5928 (Manager Bai)
Company Address: No. 18, Changzhufu Road, Changsha Economic and Technological Development Zone, Hunan Province