
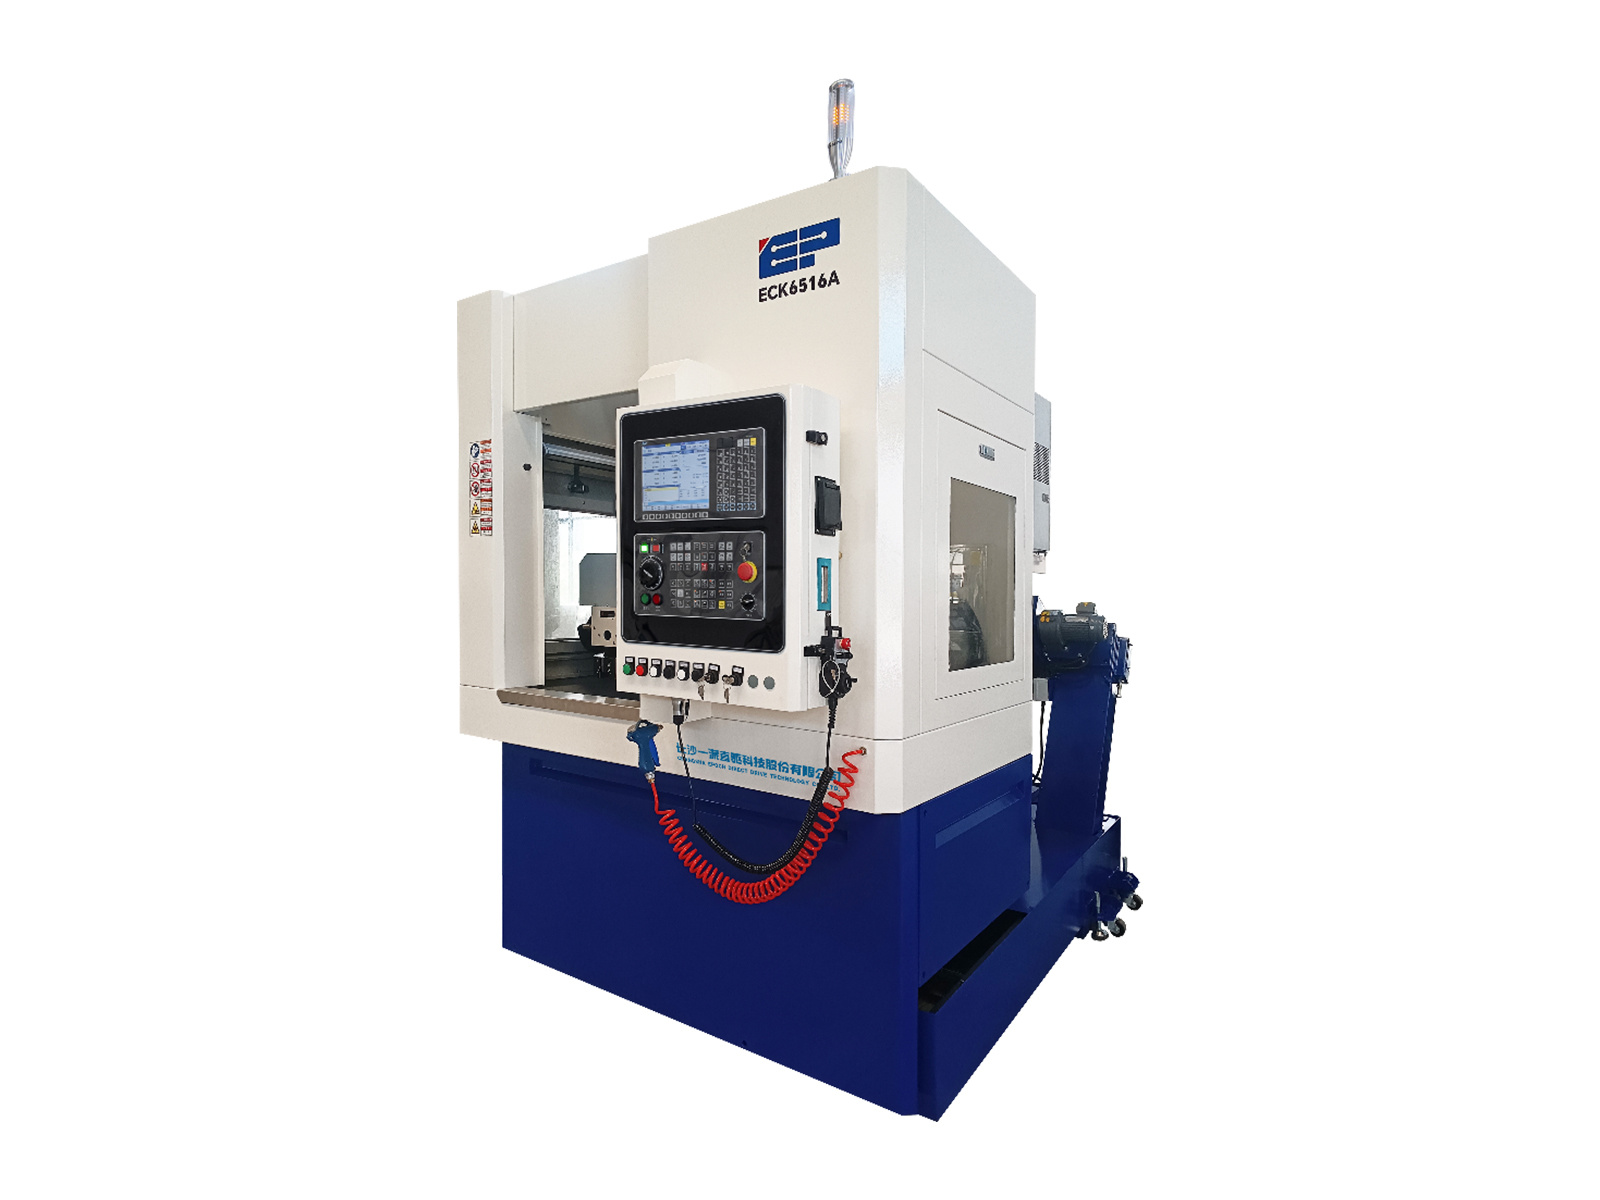
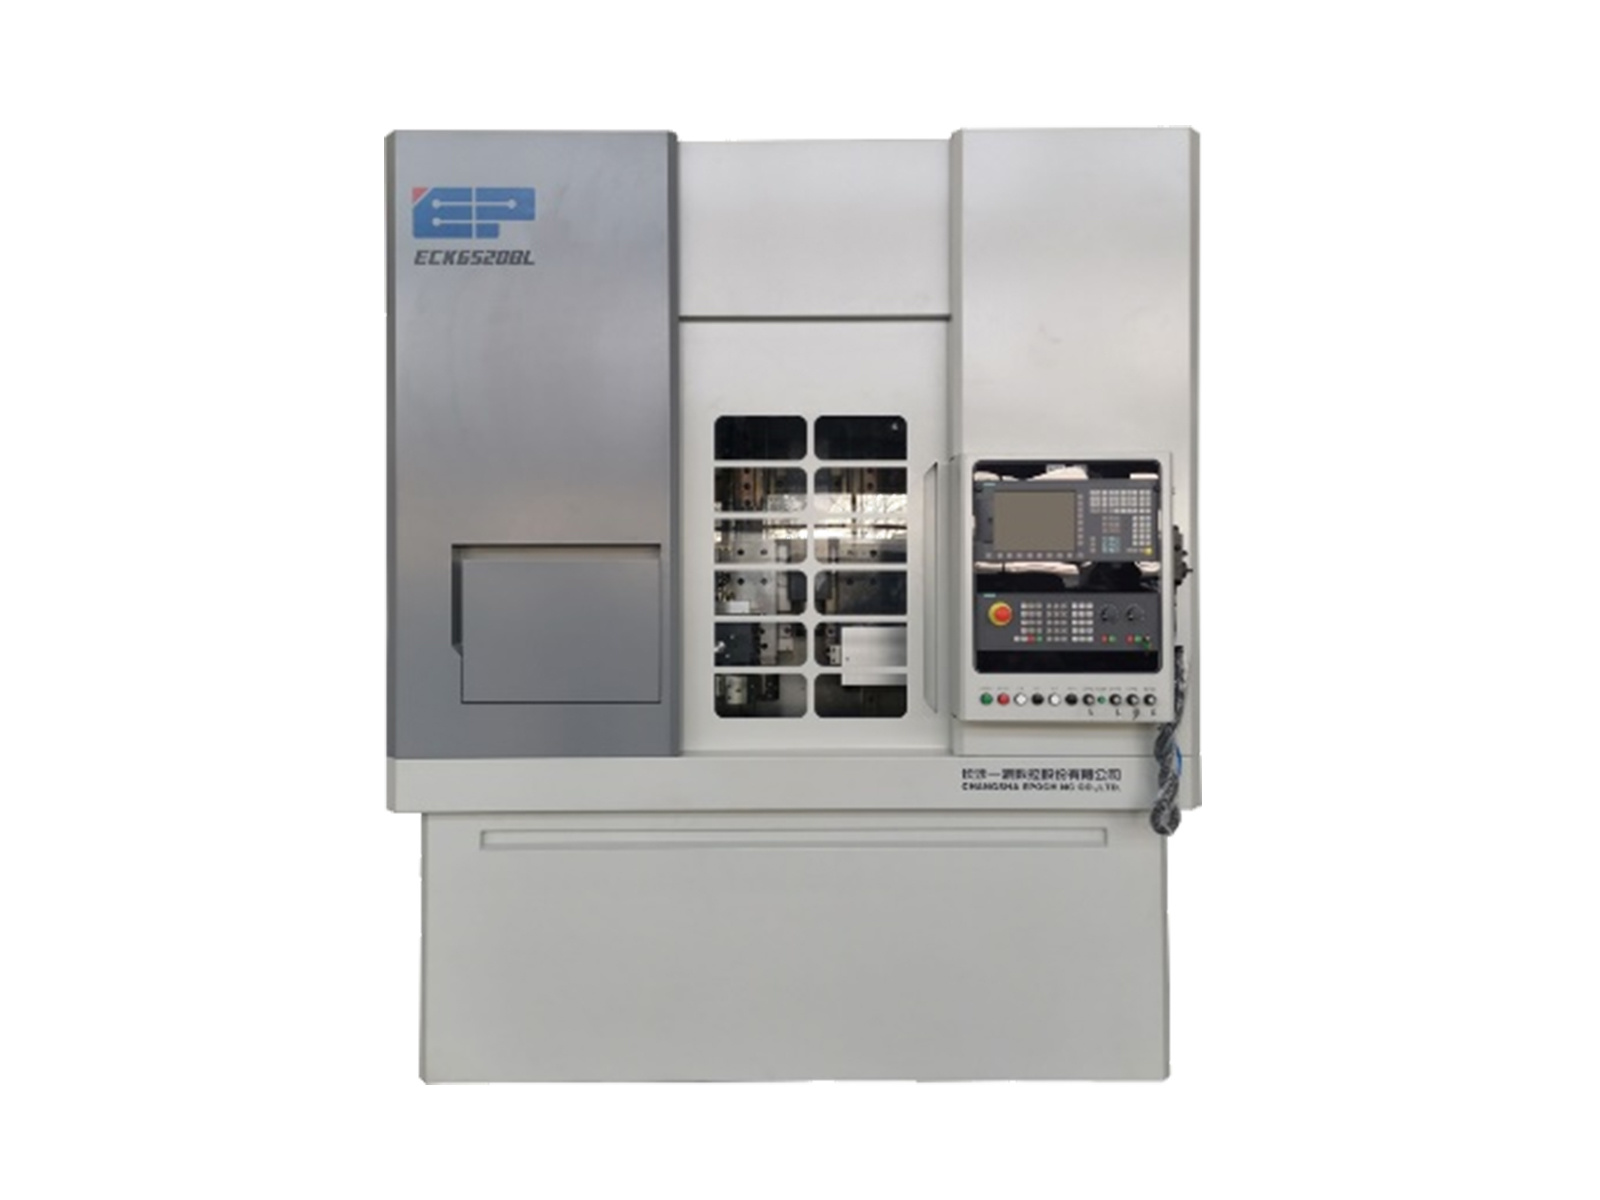
ECK6520A Turning Machine
The machine tool adopts a vertical double-column, double-Z-axis layout and a dual-channel CNC system. The left and right tool turrets are each equipped with an eight-station rotary turret, allowing for simultaneous three-axis machining of the workpiece.
It is mainly used for the rough and finish machining of aluminum and steel pistons, including the outer circle, ring groove, top surface, combustion chamber, and internal cooling oil passages.
The machine tool provides a robot interface and can be optionally equipped with an automated unit according to customer requirements.
- Technical Parameter
- Describe
-
- Commodity name: ECK6520A Turning Machine
Serial Number Item Unit ECK 6520A 1 Piston Diameter mm Φ60~Φ200 2 Piston Length mm 60~200 3 Spindle Type A2-6 bearing spindle 4 Spindle Accuracy mm 0.003 5 Spindle Speed rpm 50~1750 6 Turret 8-station servo turret (2 sets) 7 Numerical Control System SIIMENS 828D 8 Z-axis stroke mm 200 9 X-axis stroke mm 150 10 Tailstock stroke mm 4.0 11 Maximum workpiece outline (diameter) mm 200 12 Machining roughness μm Ra0.8 13 Process capability index IT7 level CmK≥1.33 14 Main unit (length × width × height) mm 2000×1500×2500 15 Net weight of main unit kg 5000 16 Total power Kw 30 -
Main Machine Configurations:
1. Basic ComponentsThe machine's base, saddle, headstock, and other basic components are made using high-strength casting technology, resulting in a stable internal microstructure. The casting structure has undergone machine dynamics and finite element analysis to optimize its geometry and ensure high rigidity. The wide and sturdy machine base, with its full-support load design, adheres to advanced material mechanics design principles, ensuring load capacity during machining.
2. High-Precision Spindle UnitUtilizes a Taiwan high-precision bearing rolling spindle A2-8, configured with a 1PH8137 spindle servo motor (Taiwan servo spindle motor optional). It offers high precision, long lifespan, and easy maintenance.
3. Linear AxesThe Z1/Z2/X1/X2 axes all use high-precision ball screw pairs and imported high-precision linear rolling guides. The Z1/Z2 axes use Rexroth 55mm roller linear guides, while the X1/X2 axes use Rexroth 45mm roller linear guides. The ball screws employ a pre-tensioned assembly process, significantly increasing transmission rigidity and eliminating thermal deformation during high-speed movement, thus ensuring the machine's positioning accuracy, repeatability, and stable machining precision. A high-precision spindle encoder (synchronous belt drive) is installed on the Z1 axis to provide the Z1 axis position signal to the linear servo tool holder drive.
4. Eight-Station Servo TurretThis machine is equipped with two eight-station servo turrets, offering good rigidity and suitability for heavy cutting.
5. Numerical Control (NC) and Electrical Control Systems(1) Employs a Siemens 828D dual-channel numerical control system, which is user-friendly and highly reliable;
(2) Wiring within the electrical cabinet complies with national electrical safety standards, ensuring the control system is free from external interference during operation. An air conditioner is used to quickly exhaust hot air from the electrical cabinet, maintaining a constant temperature and ensuring long-term stable operation of the control system.
A timed and metered (adjustable) automatic lubrication system automatically supplies oil to the guide rails, screws, and other moving parts, reducing waste and preventing environmental pollution.
6. TailstockThe hydraulically driven tailstock sleeve moves to extend or retract the center point, with separate feed and rapid traverse functions, and adjustable clamping force.
7. ToolingUses a piston stop as the positioning datum. The piston clamping on this machine offers two methods: hydraulic tailstock clamping and hydraulic tightening. Users can choose a combination based on their process requirements. An air-injected rotary cylinder is used, and the piston tooling stop can undergo air tightness testing.
8. OtherThe machine is equipped with a fully enclosed protective cover, a high-flow cooling system, and is aesthetically pleasing, safe, and leak-proof. The chip removal device is simple, environmentally friendly, practical, and reliable.

Direct Drive Business:86 181-6366-2916 (Manager Jiang)
Machine Tool Business:86 150-7465-5928 (Manager Bai)
Company Address: No. 18, Changzhufu Road, Changsha Economic and Technological Development Zone, Hunan Province