
ECK2150A Oval Turning Machine
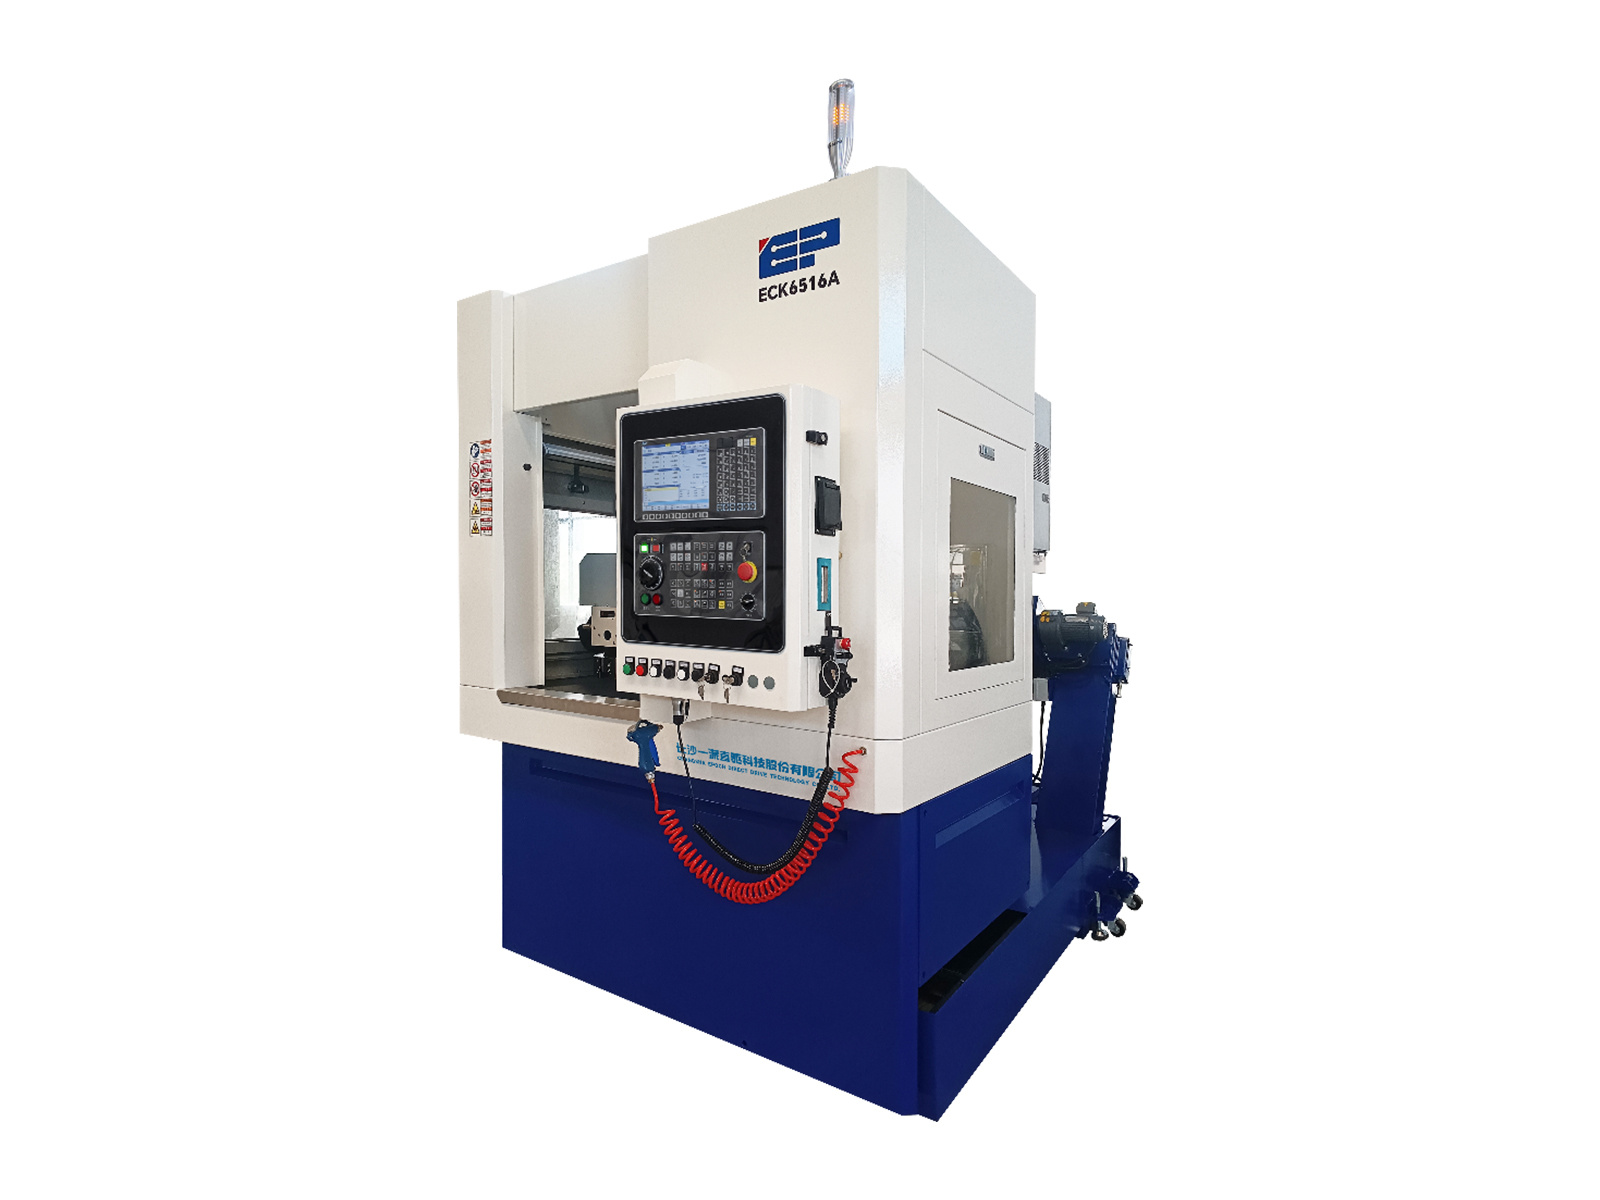
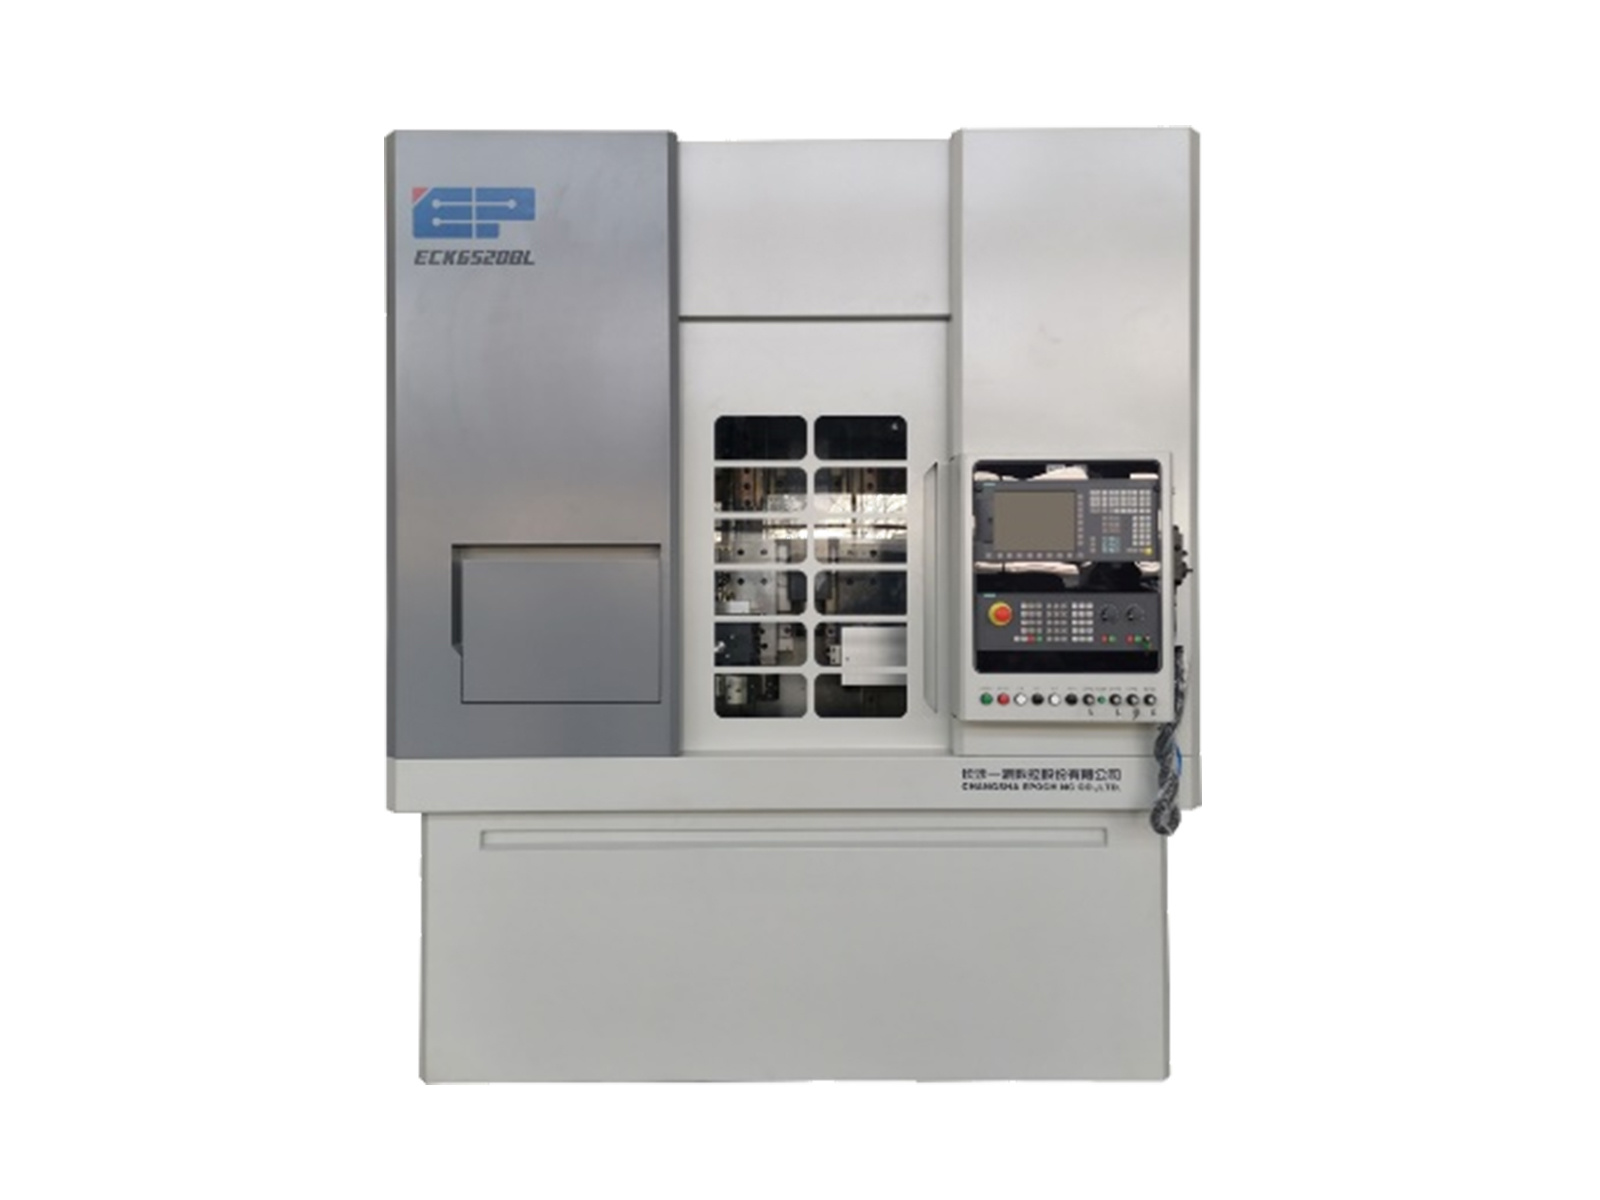
The machine tool adopts a horizontal integral flat bed structure, mainly used for machining piston irregular outer circles and piston three-dimensional abutment molds;
The software is powerful and can edit various irregular outer circles required by the piston, including standard ellipses, superimposed eccentric circles, eccentric ellipses, rotating ellipses, or discrete data fitting, etc.;
Tightening devices can be optionally selected according to customer requirements.
- Technical Parameter
- Describe
-
- Commodity name: ECK2150A Oval Turning Machine
Serial Number Item Unit ECK 2150A 1 Piston Diameter mm Φ200~Φ500 2 Piston Length mm 200~750 3 Spindle Type A2-11 Bearing Spindle 4 Spindle Accuracy mm 0.003 5 Spindle Speed rpm 10~1500 6 Linear Servo Tool Post Flat Linear Servo Tool Post System EJX1260A 7 Numerical Control System SIIMENS 828D 8 Linear Motor Stroke mm 6 9 Linear Motor Repeat Positioning Accuracy mm 0.0003 10 Maximum Workpiece Ovality (Diameter) mm 4.0 11 Maximum Workpiece Roundness (Diameter) mm 4.0 12 Machining Roughness μm Ra0.8 13 X-axis Drive Mode Servo Drive Closed-loop Control 14 Process Capability Index ΦD±0.015mm CmK≥1.33 15 Main Machine (Length×Width×Height) mm 4640×2400×2350 16 Main Machine Net Weight kg 15000 17 Total Machine Power Kw 40 -
Main Machine Configurations:
1. Basic ComponentsThe machine bed is integrally cast. The bed ways are arranged at a 45° inclination, providing a large load-bearing cross-section, good rigidity, and vibration absorption, ensuring high-precision cutting processing.
2. High-Precision Spindle UnitThis machine uses a high-precision bearing spindle A2-11; stepless speed regulation with high precision, long life, and easy maintenance.
3. SlideThe machine's Z, X1, and X2 axes use 55mm linear roller guides. The X1 and X2 axis slides are arranged parallel to the Z-axis. The X1 axis is equipped with a linear servo tool post system (U-axis) for processing the piston outer circle into an ellipse; the X2 axis is equipped with an eight-station rotary hydraulic turret (B-axis) for processing the piston ring groove and piston top surface. The Z, X1, and X2 axes are all driven and controlled by servo motors. The X1 axis is equipped with a precision grating ruler for closed-loop control; the Z-axis is equipped with a second encoder to provide the Z-axis longitudinal position signal to the linear servo control board.
4. Linear Servo Tool Post(1) The new generation of flat linear servo tool post EJX1260A, independently developed, has reached the international advanced level. This tool post has extremely high dynamic accuracy, dynamic stiffness, and frequency response. The maximum output of the servo tool post reaches 1500N, the stroke is ±3mm, and the repeat positioning accuracy is as high as 0.0003mm.
(2) Uses a high-precision servo driver EHA3020T0S with dual-CPU control, independently developed, with a servo frequency of up to 16K.

5. Numerical Control System and Electrical Control System
(1) Machine Numerical Control System
Equipped with a high-performance Siemens 840D SL numerical control system, configuring corresponding servo motors, servo drivers, PLCs, etc., according to the axis requirements; installing "YiPai ECK2150A Piston Surface Data Processing Software V1.0" for processing piston surface data; using a high-precision servo driver with independently developed dual-CPU control to achieve piston elliptical control processing.
(2) Machine Electrical System
The machine's electrical design complies with GB-5226.1 electrical standards.
The power circuits have overcurrent and short-circuit protection. All machine-related actions have corresponding interlocks to ensure equipment and personal safety.
The electrical system has a self-diagnostic function. Operators and maintenance personnel can observe the operating status of various parts of the machine at any time according to indicator lights and displays.
Main electrical components are selected from imported products from Japan and Germany. Other electrical components are selected from products of Sino-foreign cooperation to ensure the safety and reliability of the machine.(3) Electrical Cabinet
The electrical cabinet is fully enclosed, with air conditioning for heat dissipation, and the protection level reaches IP54 requirements.
6. TailstockThe tailstock is located on the right side of the bed. The tailstock body can be connected to the Z-axis as one unit and moved left and right along the spindle axis by the Z-axis servo motor to meet the processing of pistons of different lengths. The tailstock hydraulic pressure is visible.
7. FixtureA hollow rotary hydraulic cylinder is installed at the rear of the spindle to tighten the piston. A combination of tightening and tailstock sleeve clamping can also be used to ensure the reliability of piston positioning and clamping.
8. Lubrication SystemThis machine uses a timed and quantitative (adjustable flow) automatic lubrication system to automatically supply lubricating oil to the guide rails, screws, and other moving parts, reducing waste and preventing environmental pollution.
9. OthersThe machine is equipped with a fully enclosed protective cover, a high-flow cooling system, which is beautiful, safe, and leak-proof. The chip removal device is simple, environmentally friendly, practical, and reliable.
Direct Drive Business:86 181-6366-2916 (Manager Jiang)
Machine Tool Business:86 150-7465-5928 (Manager Bai)
Company Address: No. 18, Changzhufu Road, Changsha Economic and Technological Development Zone, Hunan Province