
ETK3810A Final Boring Machine
Used for precision machining of connecting rod big end straight holes and small end irregular holes (tapered holes, curved holes);
The machine tool has two main spindles arranged in parallel. The first main spindle adopts a high-precision hydrostatic-dynamic spindle to complete the precision machining of the connecting rod big end hole. The second main spindle adopts a high-precision hydrostatic-dynamic electric spindle, equipped with a precision micro-displacement servo boring device, to complete the precision machining of the irregular pin hole surface (tapered hole, curved hole) of the connecting rod small end hole;
The micro-displacement movement of the boring bar is completed while the main spindle is rotating at high speed. It has automatic dynamic balance and can maintain high-precision and stable operation of the main spindle;
The size of the pin hole can be fine-tuned through the machine tool control program interface;
The machine tool has high machining accuracy, good accuracy stability, high machining efficiency, simple and quick operation programming, short auxiliary time, and is suitable for new product development, small batch and multi-variety production, and large batch production of a single variety.
- Technical Parameter
- Describe
-
- Commodity name: ETK3810A Final Boring Machine
Serial Number Item Unit ETK3810A 1 Processing range of connecting rod small end hole diameter mm Ф30~Ф60 2 Processing range of connecting rod large end hole diameter mm Ф50~Ф100 3 Connecting rod length range mm 220~400 4 Connecting rod large and small end hole distance range mm 180~280 5 Distance between two main spindles mm 440 6 Maximum effective offset of boring bar on one side mm 0.06 7
Roundness of straight hole mm Large end hole 0.004 mm Small end hole 0.002 8
Cylindricity of straight hole mm Large end hole 0.005 mm Small end hole 0.003 9
Process capability index Large end hole ΦD±0.017mmCmK≥1.67 Small end hole ΦD±0.011mmCmK≥1.67 10
Processed surface roughness μm Large end hole Ramax1.6μm μm Small end hole Ramax0.63μm 11 Center distance dimensional accuracy mm ±0.025mm 12 Main unit (length × width × height) mm 3100×1860×2200 13 Net weight of main unit Kg 5500 14 Total machine power Kw 25 -
Main Machine Configurations:
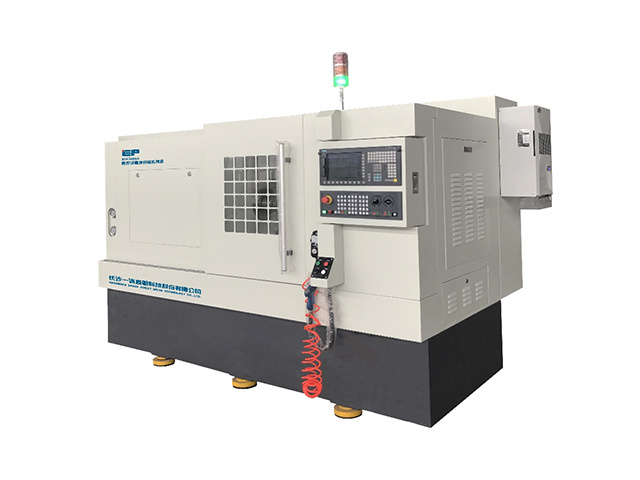
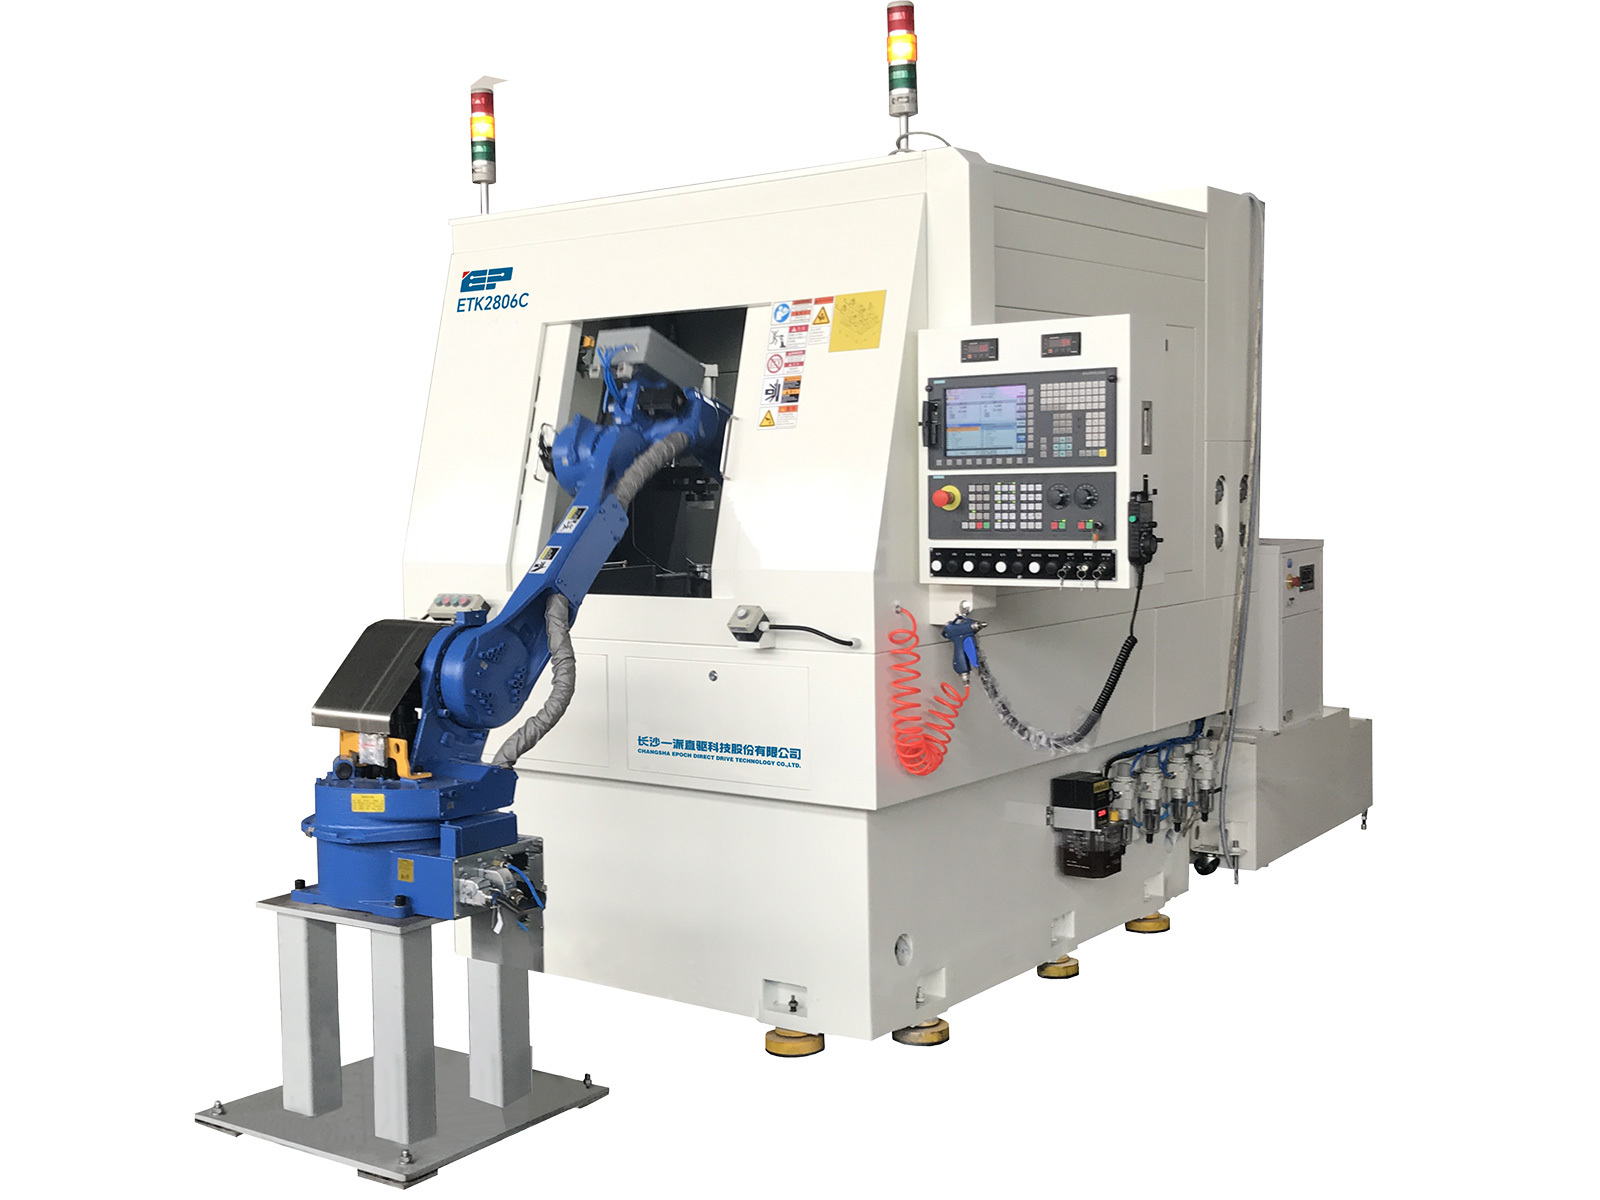
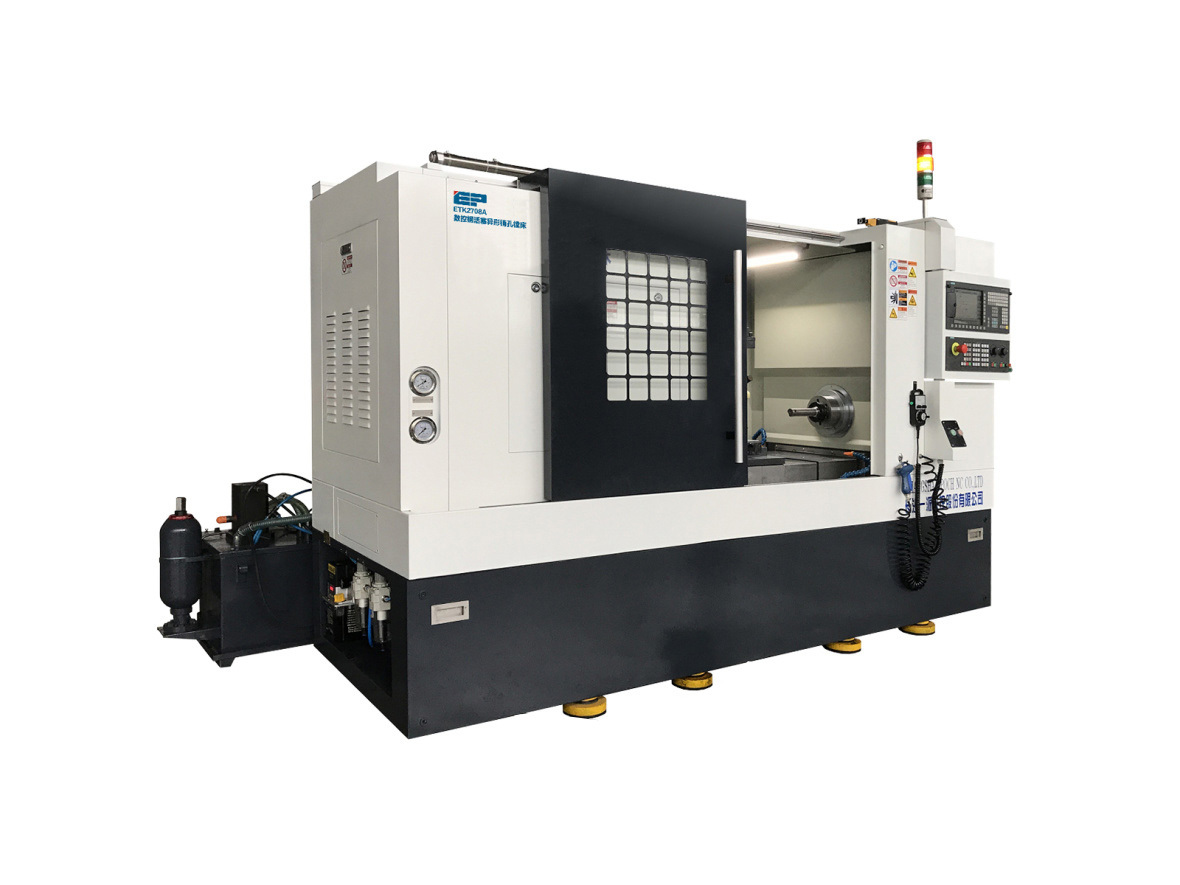
1. Basic ComponentsThe machine tool adopts a wide-body integral bed design. The machine base, spindle box base, and worktable slide, etc., are all made using high-strength casting technology, with a stable internal metallographic structure. The casting structure has undergone machine tool dynamics analysis and finite element analysis, and with the appropriate matching of reinforcing ribs, it ensures the high rigidity of the mechanical components and can ensure the needs of high-precision machining.
2. Spindle UnitThe machine tool adopts a dual-spindle structure. The first spindle adopts a high-precision hydrostatic spindle, driven by a Siemens servo spindle motor, with a parking angle orientation function; the second spindle adopts a high-precision hydrostatic electro-spindle, using an inverter or CNC system for stepless speed regulation. The spindle oil supply system is equipped with a constant temperature oil tank to maintain the high precision of the machine tool.
3. Linear AxisThe machine tool's X-axis, Y-axis (radial servo), and Z-axis are all driven by Siemens AC servo motors.
The X-axis is configured with a high-precision ball screw and imported high-precision linear rolling guide rails, and a high-precision linear grating ruler is added to form a closed-loop control.
The Y-axis is configured with a micro-displacement servo boring bar device (a patented product of Yipai CNC), which completes the machining of the connecting rod small head irregular hole surface (tapered hole, curved hole). The diameter and shape of the small head pin hole can be finely adjusted through the machining program. The micro-displacement movement of the boring bar is completed under the high-speed rotation of the spindle.
It has an automatic dynamic balancing function, which can maintain the high precision of the spindle rotation.
The Z-axis is configured with a high-precision ball screw and imported high-precision linear rolling guide rails.
4. CNC SystemIt adopts the SIEMENS 828D CNC system. The CNC programming and automatic processing programs are all instruction code programming, with complete functions, simple operation, high reliability, and good stability. It is equipped with a portable manual operating device for convenient machine tool debugging and operation.
The wiring in the electrical cabinet complies with national electrical safety standards to ensure that the control system is not affected by external interference during operation. It is equipped with an electrical cabinet air conditioner to maintain a constant temperature in the electrical cabinet, allowing the control system to operate stably for a long time.
5. Lubrication SystemIt adopts a safe, timed, and quantitative (adjustable) automatic centralized lubrication device to perform forced lubrication on the linear guide rails and ball screws. When the oil level is too low (lack of oil), the machine tool displays an alarm.
6. Cooling and Chip Removal SystemA high-flow cooling system ensures effective cooling of the workpiece and cutting tools and smooth chip removal in the processing area. It adopts an automatic chip removal device, improving the automation level of the entire machine. Sophisticated oil-water separation equipment meets the needs of oil-water separation, preventing the deterioration of cutting fluid and extending the service life of the cutting fluid.
7. Appearance and ProtectionIt adopts a fully enclosed integral protection, with a beautiful and practical appearance. The X-axis and Z-axis adopt telescopic guide rail protective covers from well-known manufacturers, effectively protecting the moving parts and extending their service life.

Direct Drive Business:86 181-6366-2916 (Manager Jiang)
Machine Tool Business:86 150-7465-5928 (Manager Bai)
Company Address: No. 18, Changzhufu Road, Changsha Economic and Technological Development Zone, Hunan Province